

W12CNC-12*2000 Hydraulic 4 Roller Plate Rolling Bending Machine CNC Rolling Machine
US$10,000.00-30,000.00
1 Piece(MOQ)

W12CNC-12*2000 Steel Sheet Roller Machine Rolling Machine with CNC Power 4 Rollers Plate Rolling Machine
US$10,000.00-30,000.00
1 Piece(MOQ)

CNC 4 Roller Metal Plate Rolling Machine Manufacturer Sheet Rolling Machine
US$10,000.00-30,000.00
1 Piece(MOQ)

Advanced 6X2000mm Hydraulic 4 Roller Plate Rolling Machine
US$10,000.00-30,000.00
1 Piece(MOQ)

Heavy-Duty 4 Roller Sheet Metal Rolling Machine for All Metals
US$10,000.00-30,000.00
1 Piece(MOQ)

W12 CNC Hydraulic Steel Plate Rolling Machine with 4 Rollers
US$10,000.00-30,000.00
1 Piece(MOQ)
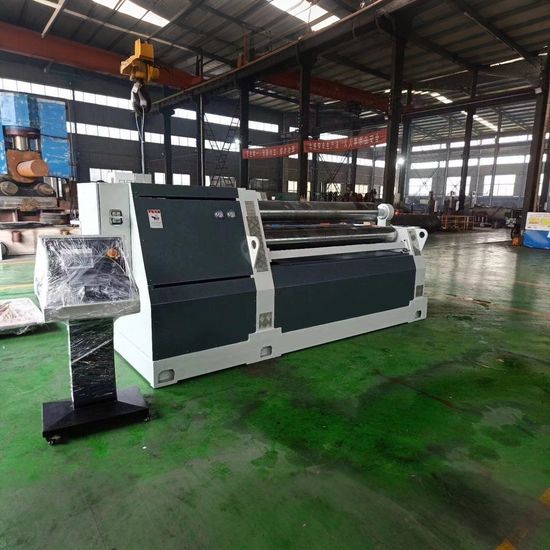
W12-16*2000 CNC Four Rollers Plate Rolling Machine
US$10,000.00-30,000.00
1 Piece(MOQ)

Hydraulic 4 Roller Plate Rolling Bending Machine CNC Rolling Machine Easy to Maintenance Decoiler
US$10,000.00-30,000.00
1 Piece(MOQ)

Four Rollers Plate Rolling Machine
US$10,000.00-30,000.00
1 Piece(MOQ)

Advanced Customized 4 Rollers Plate Bending Machine for Sale
US$10,000.00-30,000.00
1 Piece(MOQ)

W12CNC-16*2500 Four Rollers Plate Rolling Machine Safety Easy to Maintenance Decoiler
US$10,000.00-30,000.00
1 Piece(MOQ)

W12-25X2500 Nc Hydraulic Four Rollers Cone Rolling Bending Machine
US$10,000.00-30,000.00
1 Piece(MOQ)


